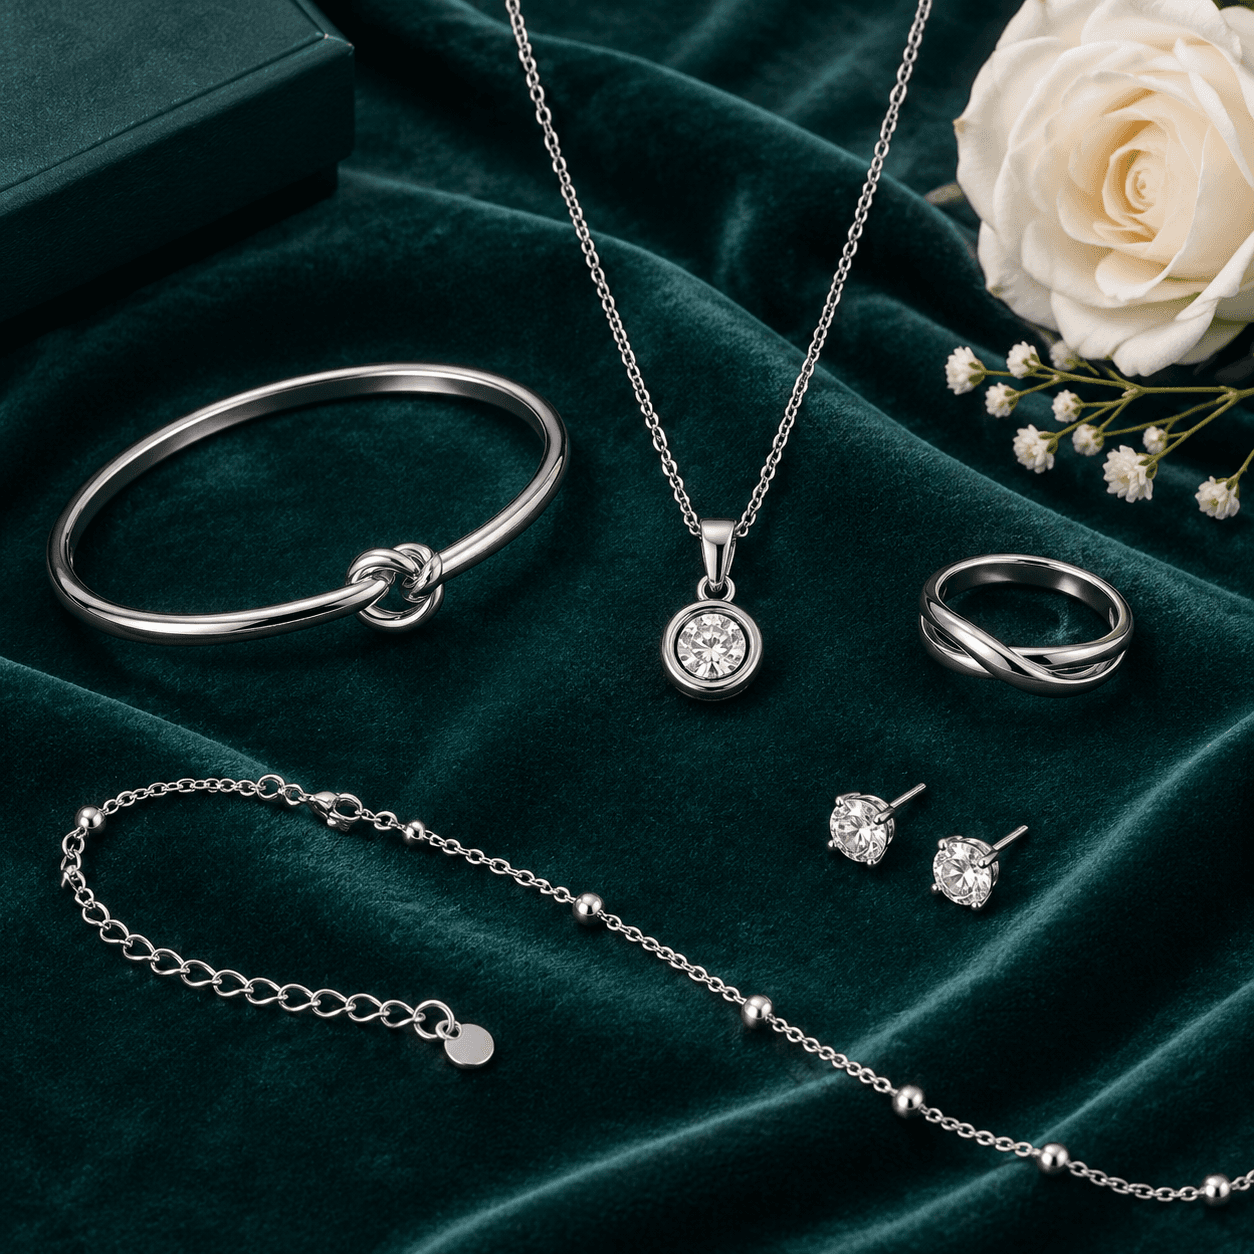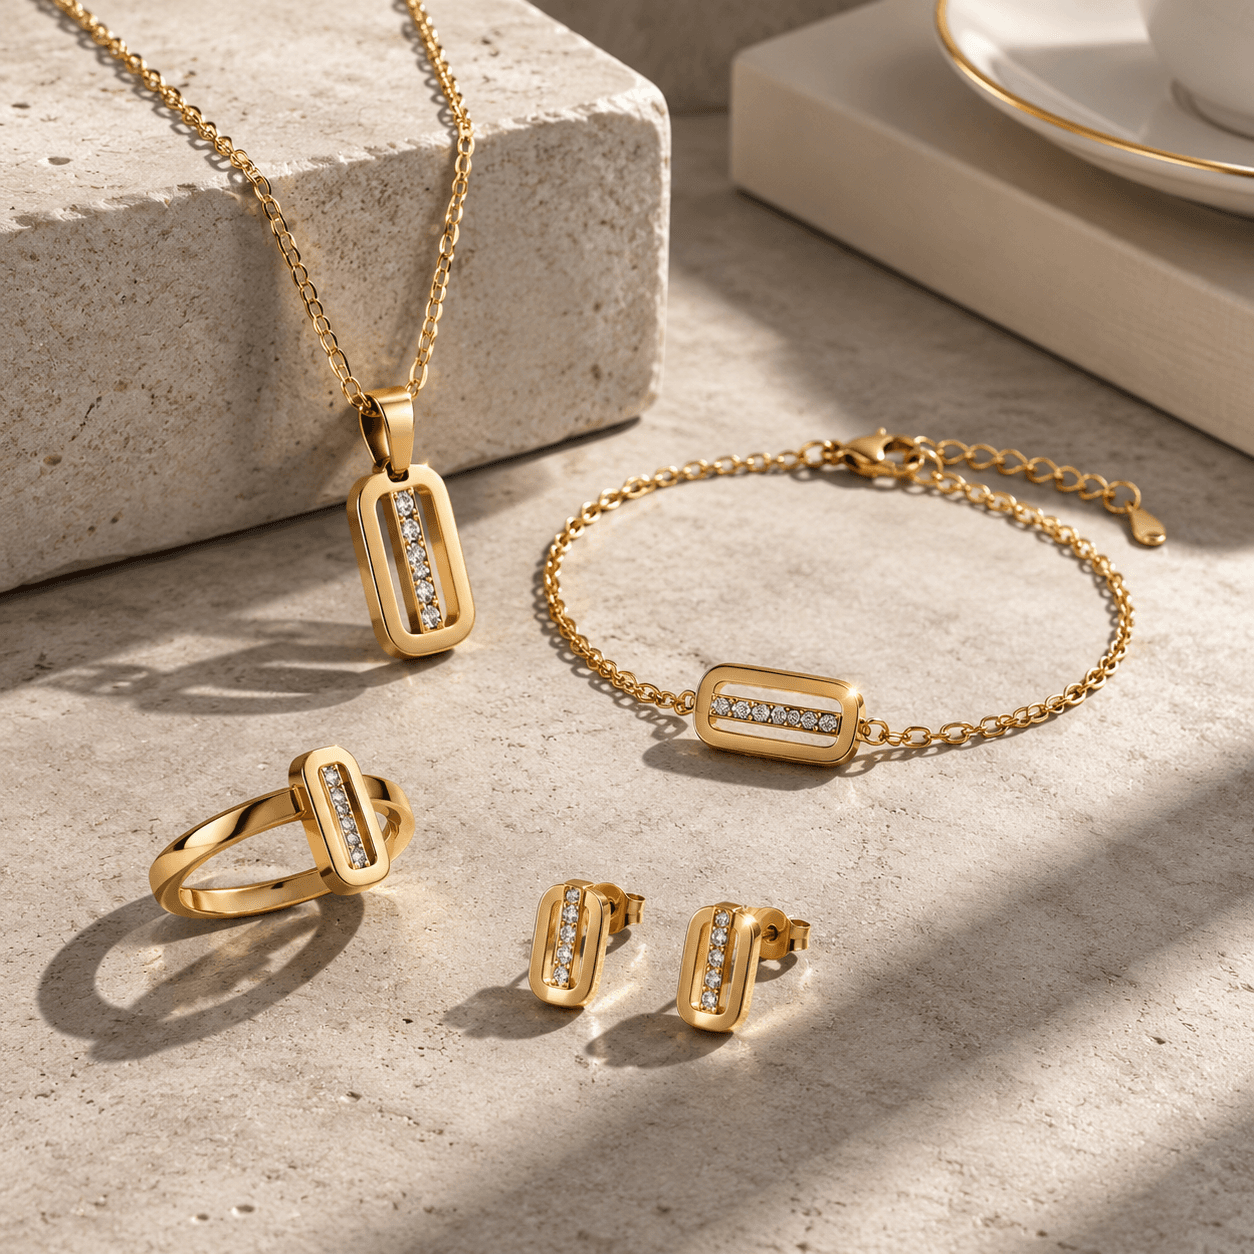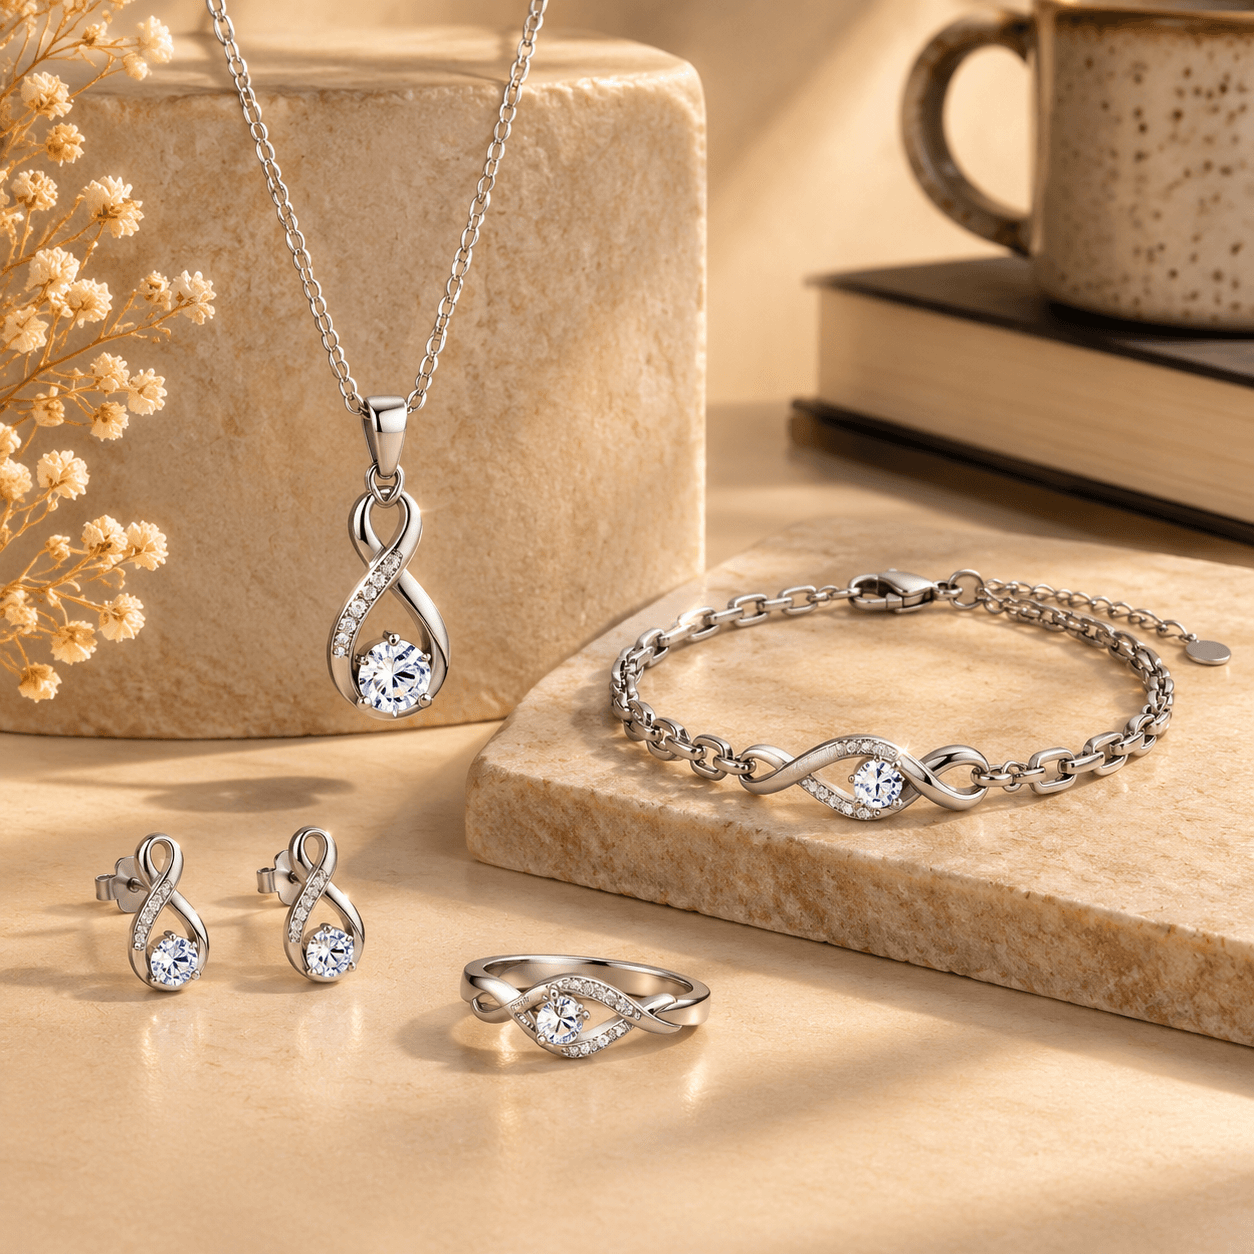
Stainless steel jewelry is often chosen for its corrosion resistance and straightforward care, but it is not completely immune to discoloration or corrosion. For jewelry designers and sourcing teams, understanding the difference between surface residue, finish wear, and damage to the underlying alloy helps set clearer material specifications and product-care guidance.
316L stainless steel is an austenitic chromium-nickel-molybdenum alloy. Its chromium supports a thin, protective passive film, while molybdenum improves resistance to localized corrosion in chloride-containing environments. These properties make 316L a useful material option for many jewelry applications, but the performance of a finished piece also depends on its design, surface condition, processing, and use environment.
Does stainless steel jewelry tarnish?
Stainless steel does not usually tarnish in the same way as metals that readily form visible surface compounds during ordinary exposure. Its corrosion resistance comes mainly from chromium, which helps form a thin, chromium-rich oxide film when the surface is exposed to oxygen. This passive film is not a decorative coating; it is a microscopic surface layer that can reform after minor damage under suitable conditions.
“Tarnish” is often used broadly to describe several different changes. A dull or discolored surface may be caused by oils, cosmetics, or cleaning residues rather than corrosion. Pitting or material loss, by contrast, can indicate corrosion. Identifying the cause matters because cleaning may remove residue, but it cannot reverse damage to the metal or a worn decorative finish.
- Surface residue: Oils, perspiration, cosmetics, or cleaning products can affect appearance without necessarily damaging the alloy.
- Discoloration: Chemical exposure, heat, or process contamination can change a surface’s appearance.
- Pitting or crevice corrosion: Localized corrosion can occur where the passive film breaks down, especially in restricted areas where moisture and corrosive substances collect.
What 316L’s composition contributes
316L is a low-carbon austenitic stainless steel. The following ranges are general reference values; exact composition limits depend on the applicable material standard. Buyers should confirm the grade and any required documentation for the actual production material.
| Element | Common composition range or limit | Role |
|---|---|---|
| Chromium | 16–18% | Supports formation of the passive oxide film. |
| Nickel | 10–14% | Stabilizes the austenitic structure and supports useful forming characteristics. |
| Molybdenum | 2–3% | Improves resistance to pitting and crevice corrosion in chloride-containing environments. |
| Carbon | 0.03% maximum | The low-carbon limit helps reduce sensitization risk under certain elevated-temperature processing conditions. |
| Iron | Balance | Principal metallic constituent. |
Chromium and passivation
Chromium is central to stainless steel’s corrosion resistance. The passive film slows reactions between the iron-based alloy and its surroundings. It can reform after minor surface damage when conditions are suitable, but passivation does not make the alloy immune to aggressive chemicals or localized corrosion.
Nickel and austenitic structure
Nickel helps stabilize 316L’s austenitic crystal structure, which is relevant to forming and manufacturing. It should not be presented as the primary source of the alloy’s passive protection; chromium plays that role.
Molybdenum and chloride exposure
Chloride ions can contribute to localized breakdown of the passive film. Molybdenum improves resistance to pitting and crevice corrosion associated with chlorides. Perspiration and seawater can expose jewelry to chlorides, but 316L is not immune to unlimited salt exposure or harsh chemical treatment.
What the low-carbon designation means
The “L” in 316L refers to its low-carbon limit. Under certain elevated-temperature conditions, carbon can combine with chromium to form carbides at grain boundaries, reducing available chromium nearby and increasing susceptibility to intergranular corrosion. Lower carbon helps limit this sensitization mechanism. The relevance depends on the manufacturing process and conditions.
Why 316L jewelry may still discolor or corrode
A material grade alone does not determine the performance of a finished piece. Environmental exposure, geometry, manufacturing, and decorative finishes all matter.
Perspiration and chloride exposure
Perspiration contains water, salts, and other compounds, with composition that varies between people and conditions. Moisture trapped around joints or small components can leave concentrated residues as it evaporates. 316L generally offers greater resistance to chloride-related localized corrosion than 304, but it is not absolute protection.
Cosmetics and cleaning products
Perfume, cosmetics, and household cleaners can leave residue or expose jewelry to chemicals outside its intended service environment. Some residues affect appearance without corroding the metal; others may affect the alloy or a decorative finish. Gentle cleaning and thorough drying are more reliable care guidance than saying stainless steel needs no maintenance.
Manufacturing and surface condition
Polishing compounds, processing residues, embedded contaminants, and handling can affect the finished surface. The nominal alloy grade alone does not guarantee a clean, consistent surface. Polishing, cleaning, and inspection are important parts of production quality.
Joints and restricted areas
Chain connections, clasps, stone settings, and other small features can retain moisture and residue. Consider drainage, cleanability, and inspection access when developing a design, particularly where components meet or form narrow gaps.
How decorative finishes affect performance
The stainless steel substrate and its decorative finish are separate considerations. Polished, uncoated stainless steel gets its appearance from the substrate. PVD finishing is a physical vapor deposition process used to apply a thin coating; in jewelry, it can provide a gold-colored or other decorative surface over a stainless steel component.
Appearance and service performance depend on factors such as substrate preparation, coating specification, geometry, processing, and subsequent handling. A decorative coating does not automatically improve every corrosion-related property of the complete piece. Scratches, exposed edges, coating defects, and wear can produce different surface conditions.
For sampling, review the finish’s color and consistency along with the construction and intended use. If a design combines PVD with enamel, stones, pearls, or other decorative components, assess the complete assembly and agree on relevant inspection requirements before production.
Material and finish decisions for B2B jewelry development
For OEM/ODM and private-label projects, specify more than “stainless steel” or “tarnish-resistant.” Align the material, design, finish, and inspection requirements with the product’s intended use.
- Define the intended environment. Describe expected wear, perspiration, occasional water contact, coastal exposure, and cleaning practices.
- Confirm the material grade. Specify 316L or another agreed grade. If documentation is required, confirm which records are available for the actual production material.
- Review component geometry. Check links, clasps, joints, settings, and attachment points for moisture retention, cleanability, and inspection access.
- Define the finish. Specify the intended color, texture, and appearance, including expectations for consistency across components and any decorative coating.
- Approve a representative sample. Review material and finish, construction, functional details, and customized features such as logo placement before bulk production.
- Agree on quality checkpoints. Depending on the product, these may include material and component specifications, surface cleanliness, finish consistency, joints and clasps, decorative elements, and packaging details.
If corrosion performance is a purchasing requirement, agree on the relevant test method, exposure conditions, acceptance criteria, and documentation expectations with the manufacturer. Do not assume a result for one material, finish, or design applies to a different production specification.
Care guidance
For routine care, gently clean jewelry with a soft cloth and mild soap and water, then dry it thoroughly. Avoid exposing finished jewelry to harsh cleaners unless compatibility has been confirmed. Care guidance should reflect the specific material and finish rather than promise that a piece will never discolor or corrode.
Conclusion
316L stainless steel resists ordinary corrosion because chromium supports a protective passive film, while molybdenum improves resistance to chloride-related pitting and crevice corrosion. Nevertheless, surface residue, harsh exposure, manufacturing conditions, complex geometry, and decorative finish wear can affect a jewelry piece’s appearance and performance.
For product developers, the practical approach is to specify the grade and finish, review the design and sample, and agree on appropriate inspection criteria. Clear requirements help an OEM/ODM manufacturer assess the project and support more consistent product development without relying on blanket claims such as “tarnish-proof.”